H-32, M.I.D.C. SATPUR, NASHIK-422007 Maharashtra, India
H-32, M.I.D.C. SATPUR, NASHIK-422007 Maharashtra, India
H-32, M.I.D.C. SATPUR
NASHIK-422007 Maharashtra, India
Year of Establishment: 1978
Our manufacturing operations follow a systematic 9-step sequence from raw polymer compounding to high-pressure hydraulic curing, CNC moulding, and computerized QA/QC proof-load testing.
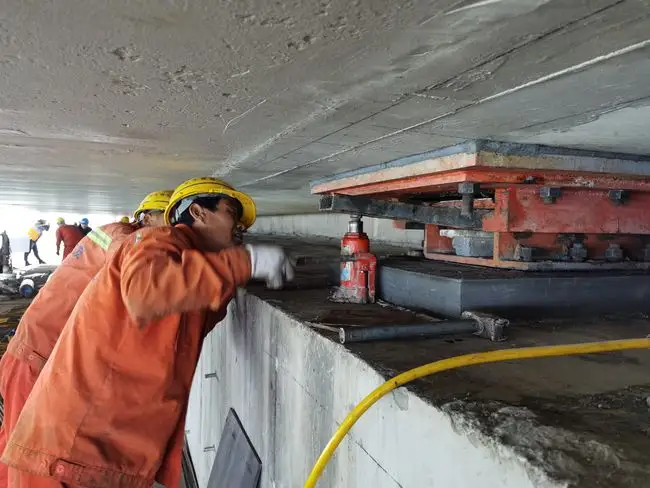
Explore the step-by-step manufacturing workflow followed for our bearing products, from material preparation and processing to final inspection. The workflow highlights the key stages involved in maintaining consistent quality, precision, and product reliability.
Incoming inspection of raw Natural Rubber (NR) / Chloroprene (CR), carbon blacks, zinc oxide, vulcanizing agents, and mild steel plates (IS:2062). NABL test certificate verification.
Precision weighing of chemicals and masterbatch mixing on heavy duty Two-Roll Open Mixing Mills to achieve homogeneous dispersion, uniform rheology, and batch-to-batch consistency.
Conversion of mixed rubber compound into continuous sheets of exact specified thickness with zero porosity and controlled dimensional tolerances using multi-roll calenders.
Steel laminates are sheared, edges radiused (R ≥ 2mm), grit shot-blasted to Sa 2.5 finish to remove scale/rust, chemically degreased, and coated with Chemlok adhesive bonding agents.
Systematic alternating stacking of primed steel laminates and un-vulcanized elastomer sheets inside heavy CNC-machined steel moulds with precise registration spacers.
Curing under high hydraulic clamping pressure (over 1000 kN) and controlled temperature (145°C - 160°C) for pre-programmed cure cycle times to ensure total molecular cross-linking and permanent bond.
Careful extraction of vulcanized bearings, flash trimming, edge smoothing, inspection of outer protective rubber layer (≥ 4mm side / 2.5mm top-bottom), and initial visual check.
Hot-embossing / stenciling of unique lot number, bearing type, dimensions, manufacturer code, and production date onto each bearing for permanent field traceability.
Proof load compressive stiffness testing, shear modulus determination, dimension verification, witness inspection by client engineers, and generation of manufacturer test certificate (MTC).
Swipe through live high-resolution images of our Nashik manufacturing line, testing frames, and curing presses.
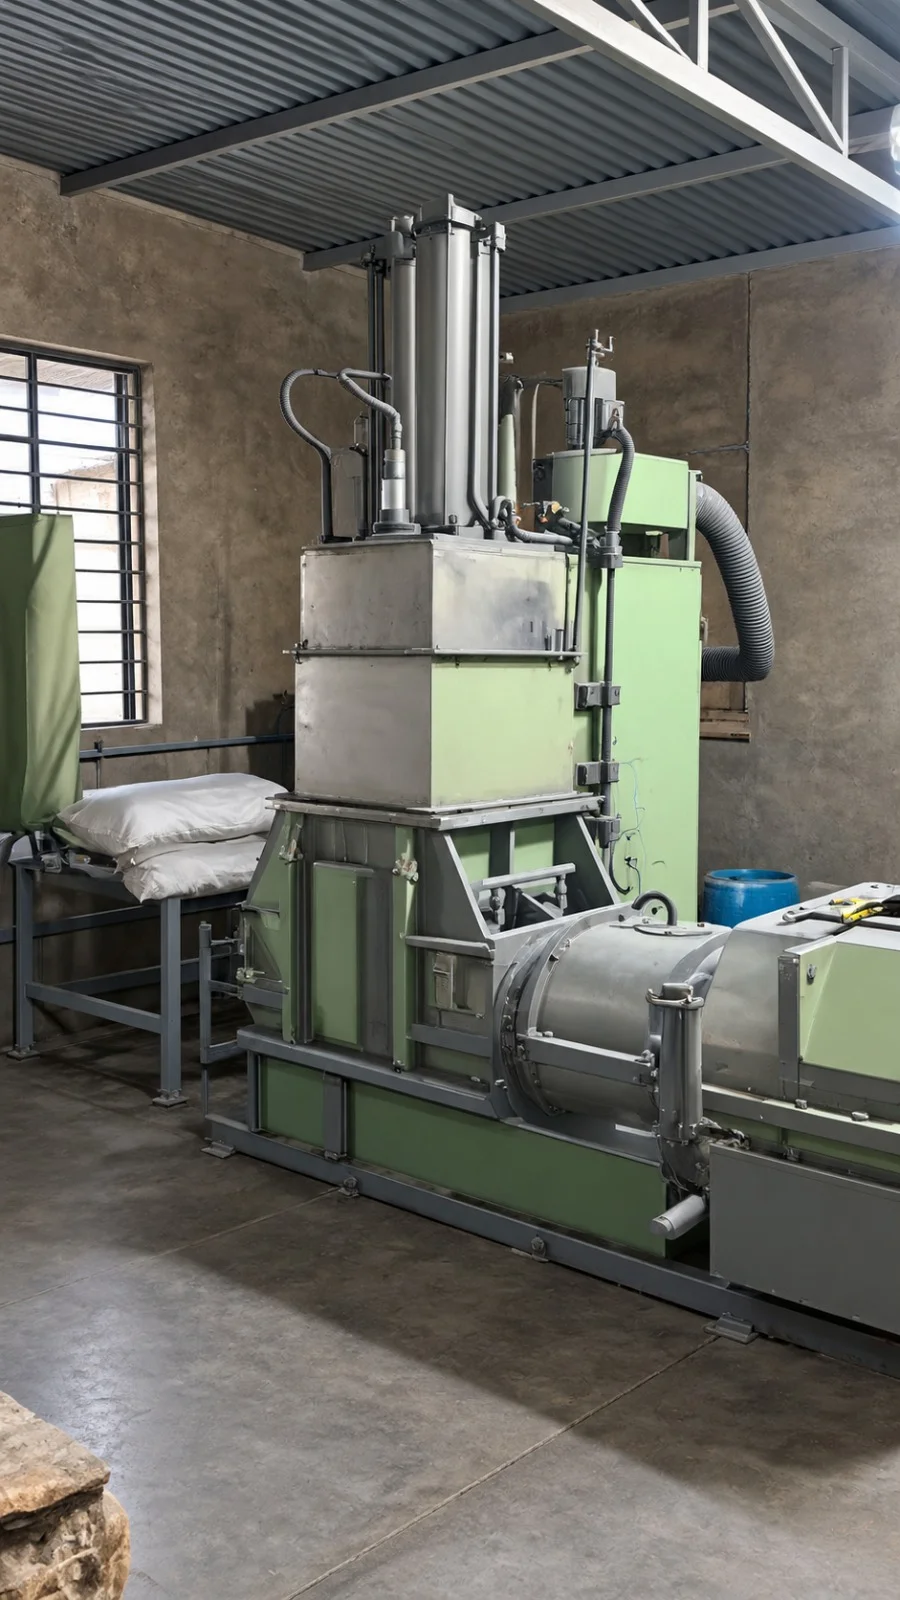
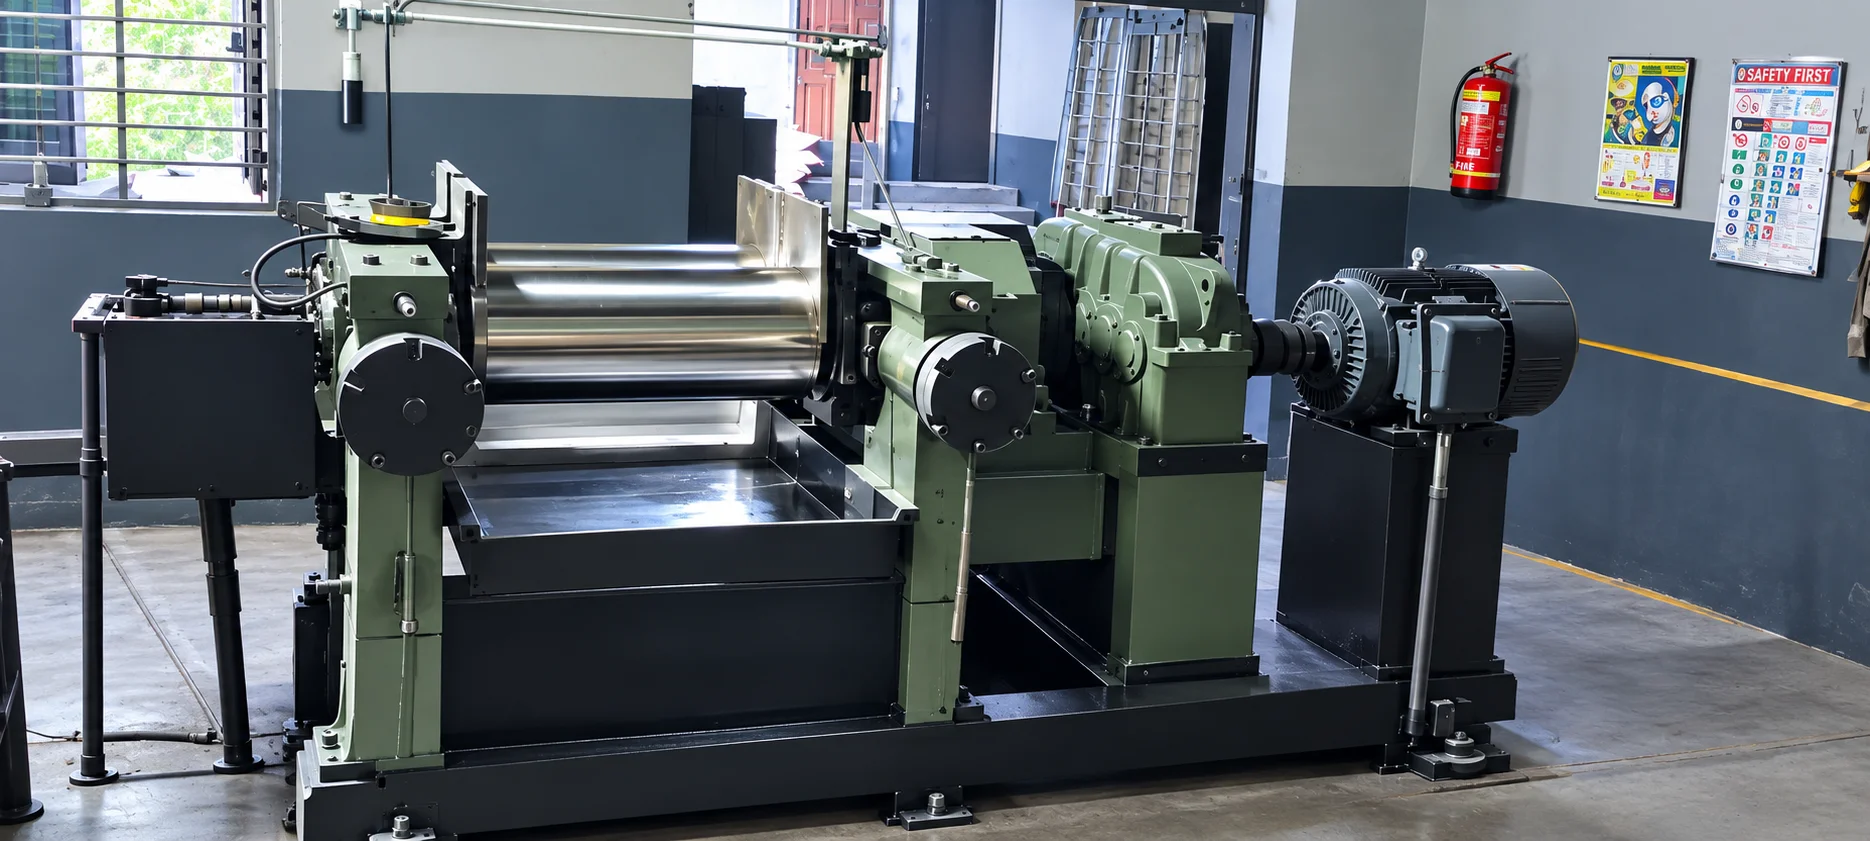
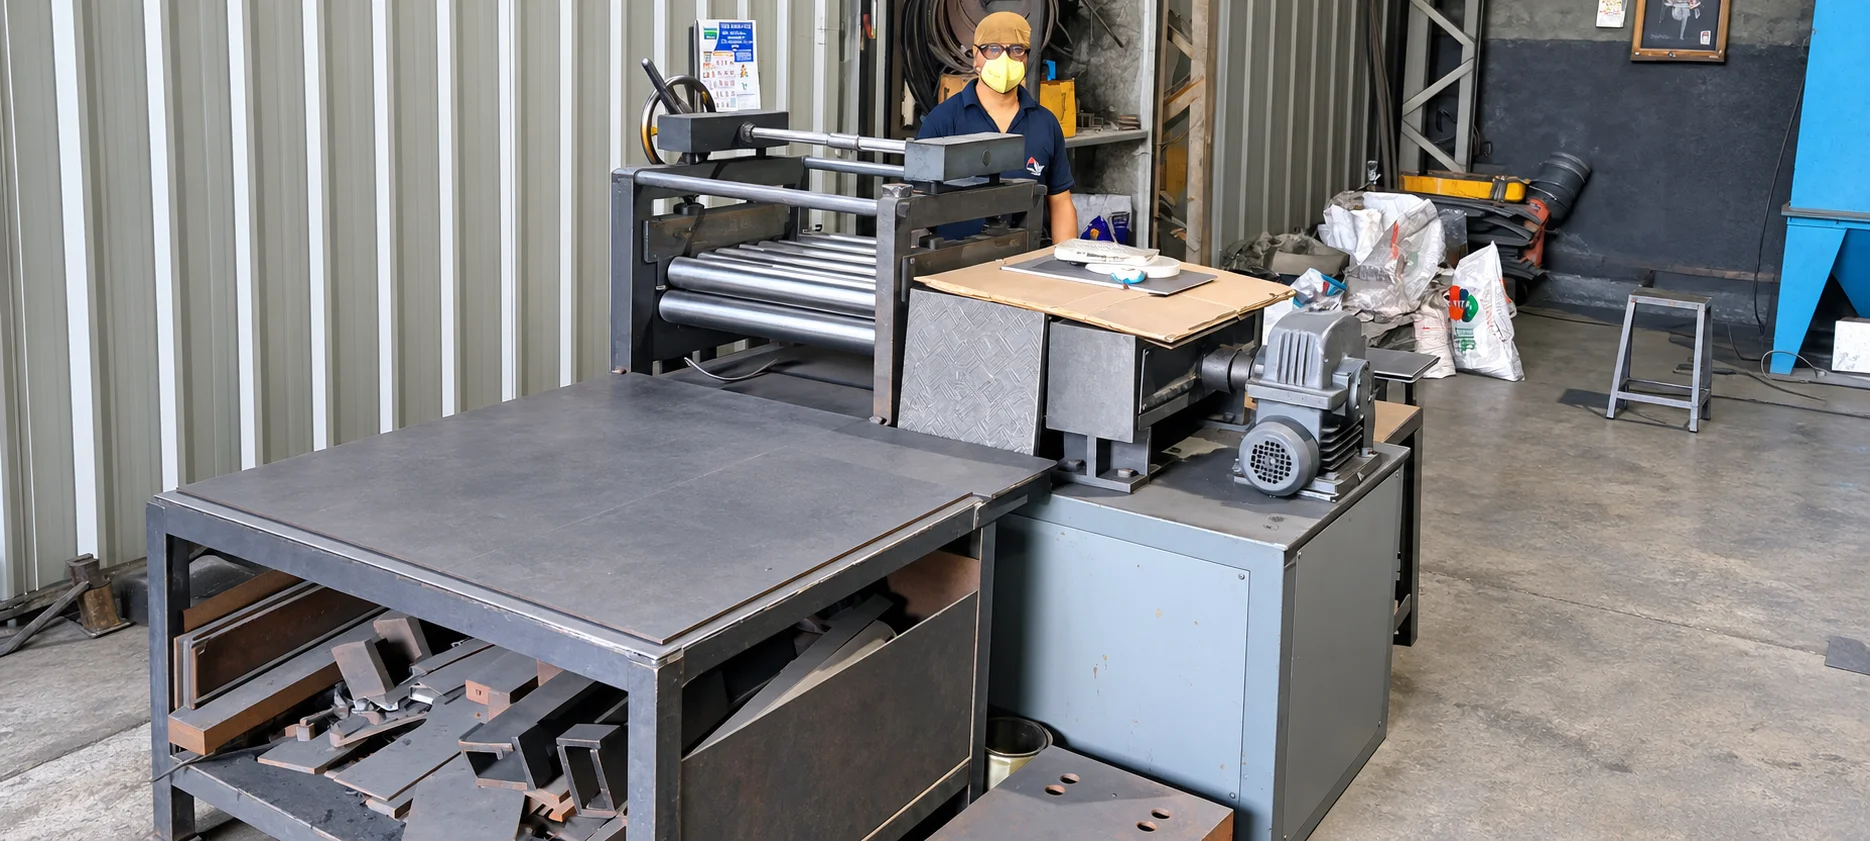
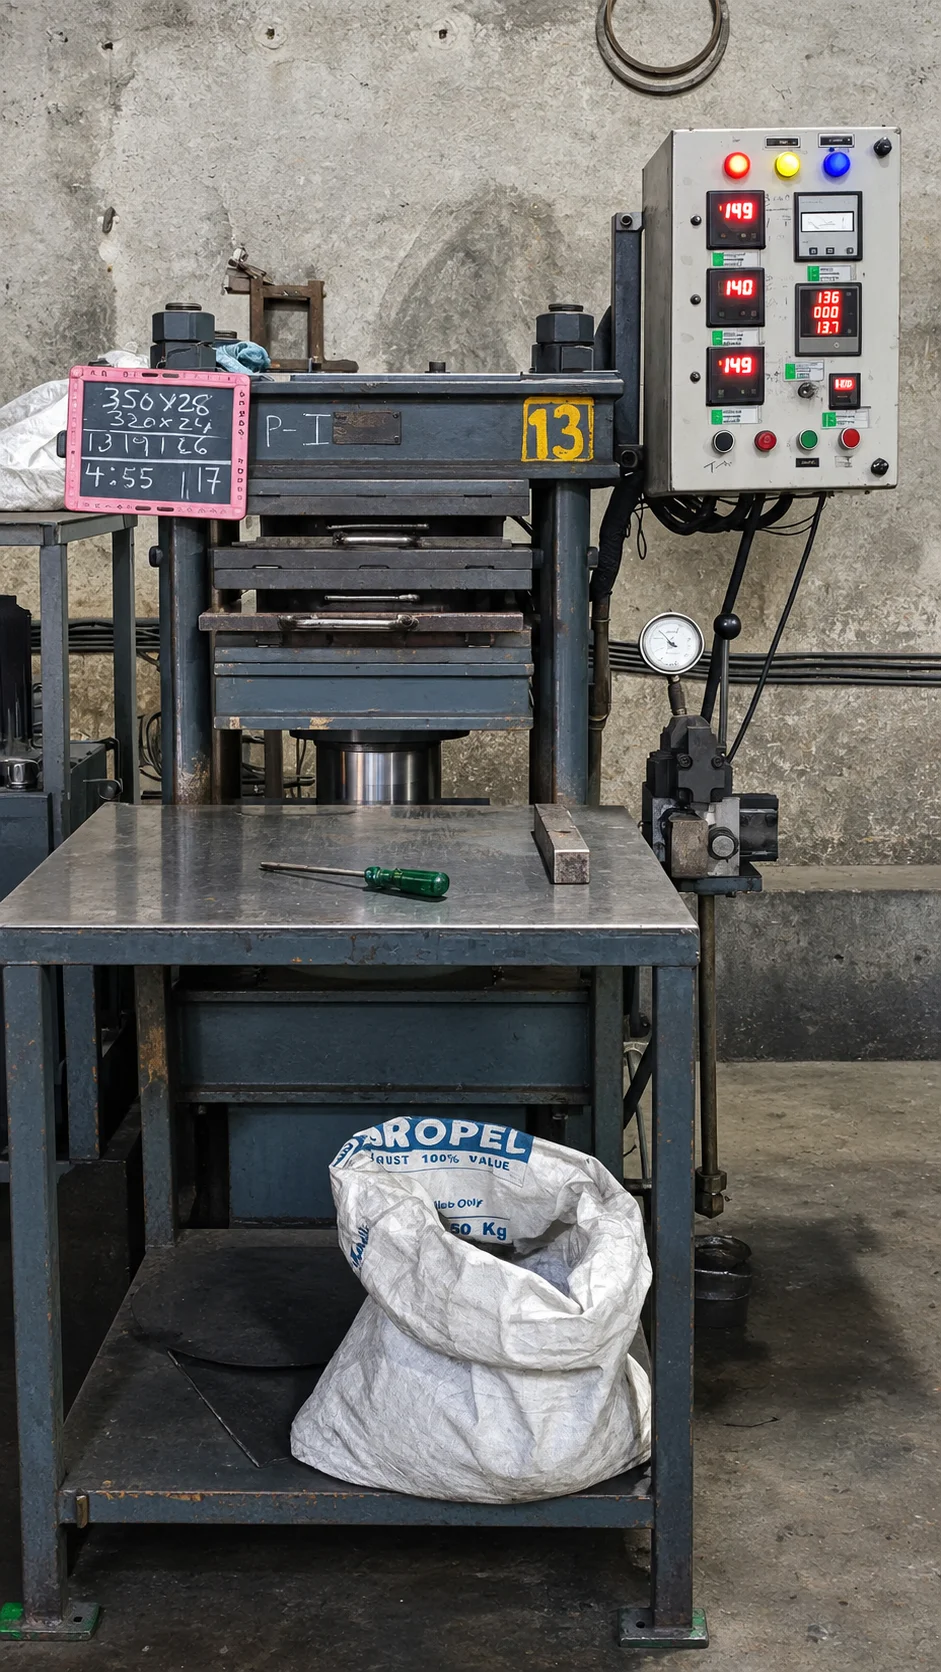
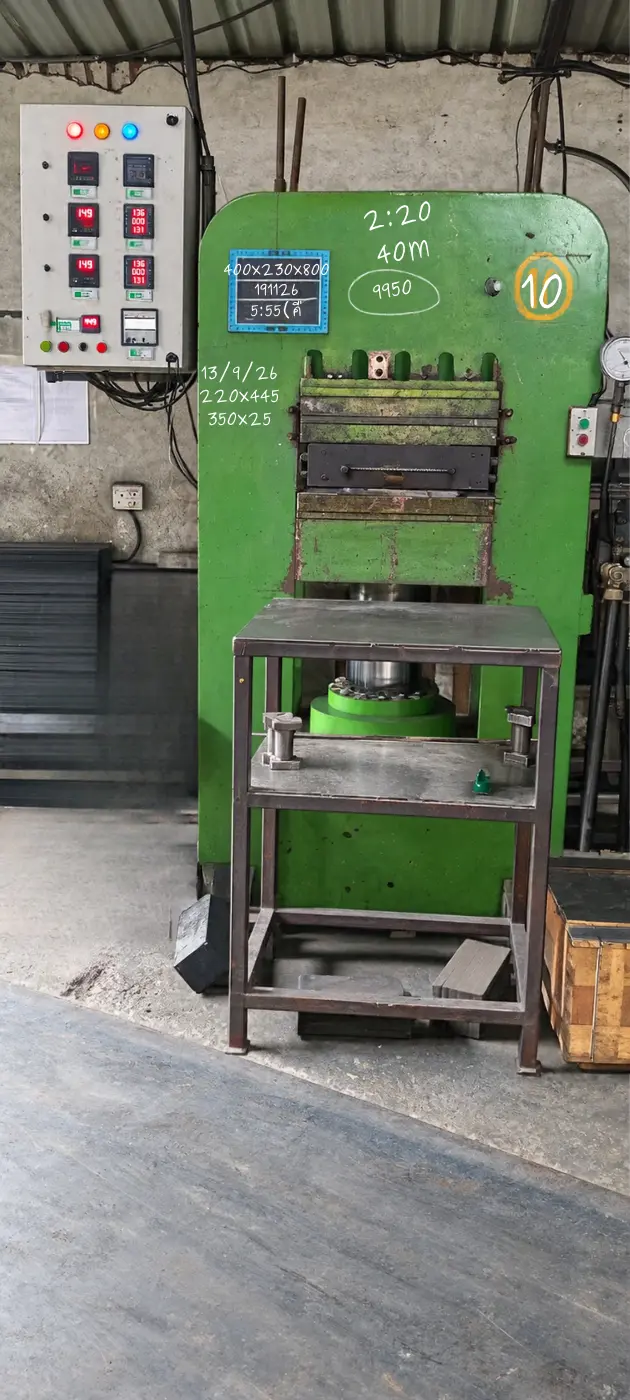
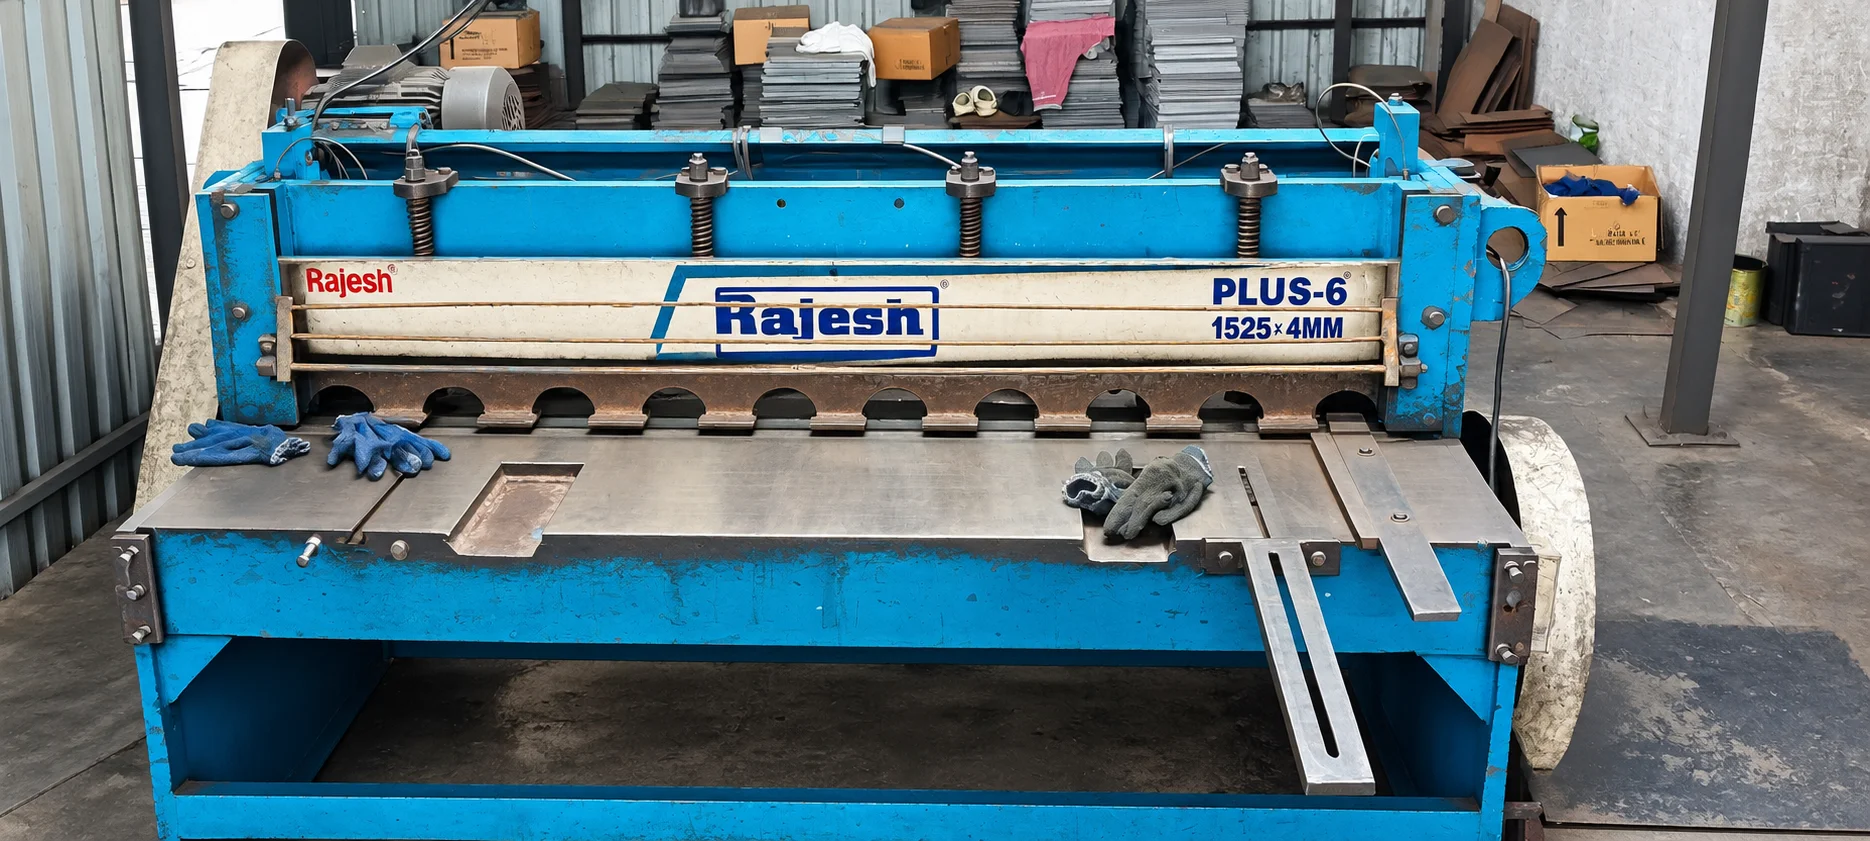
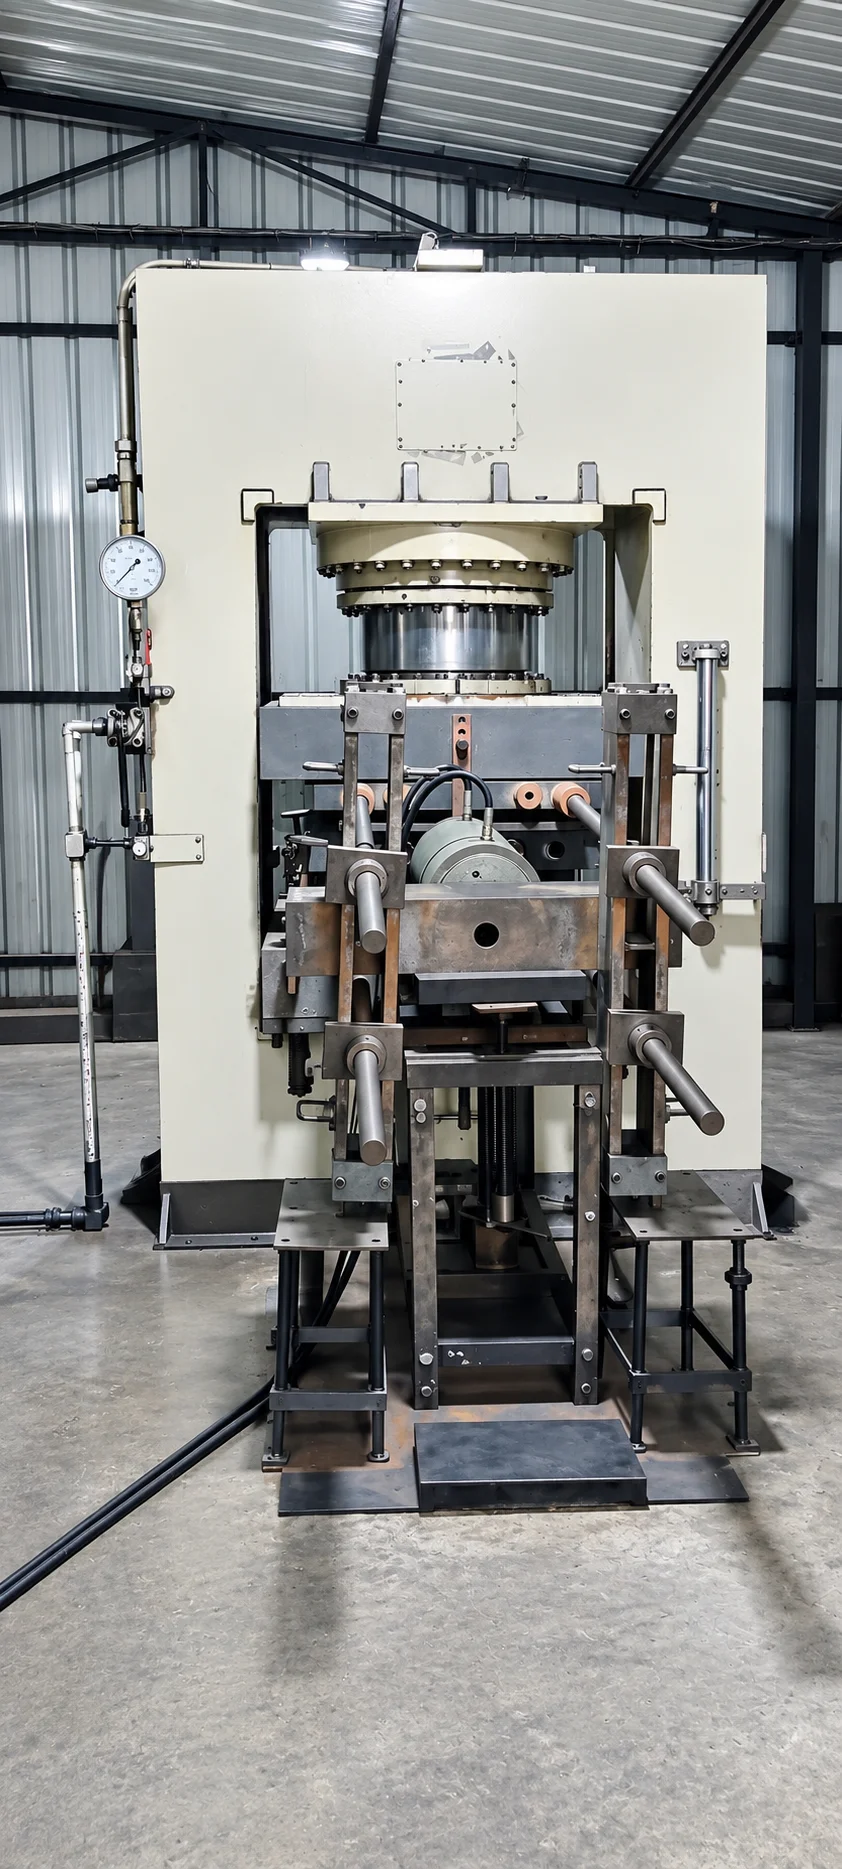
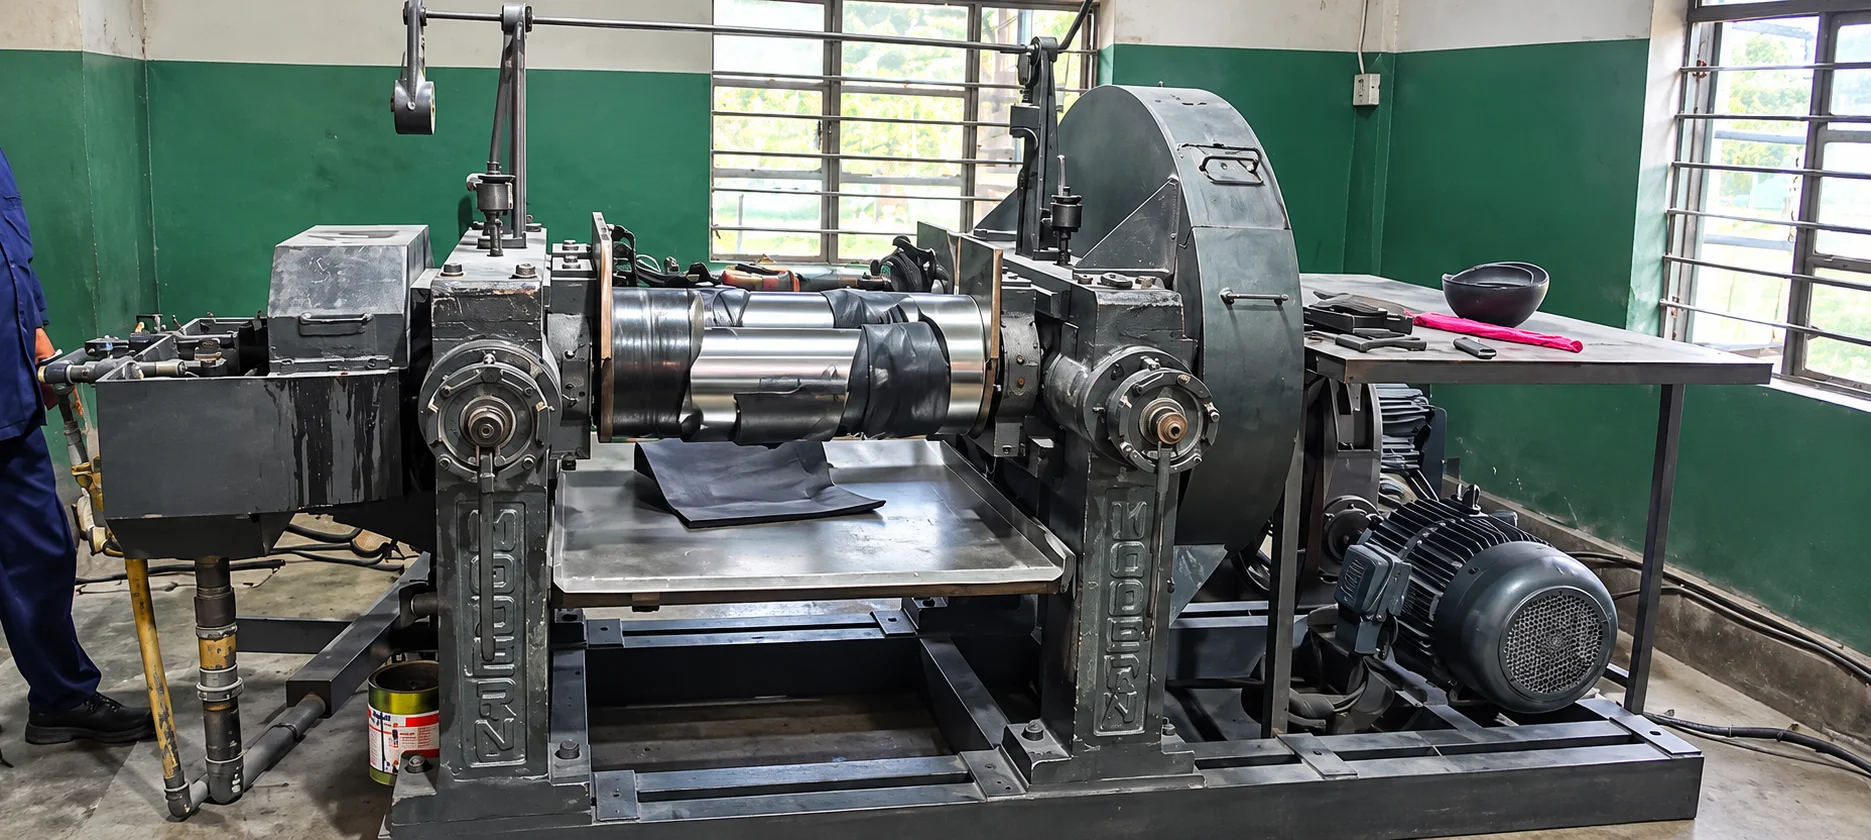
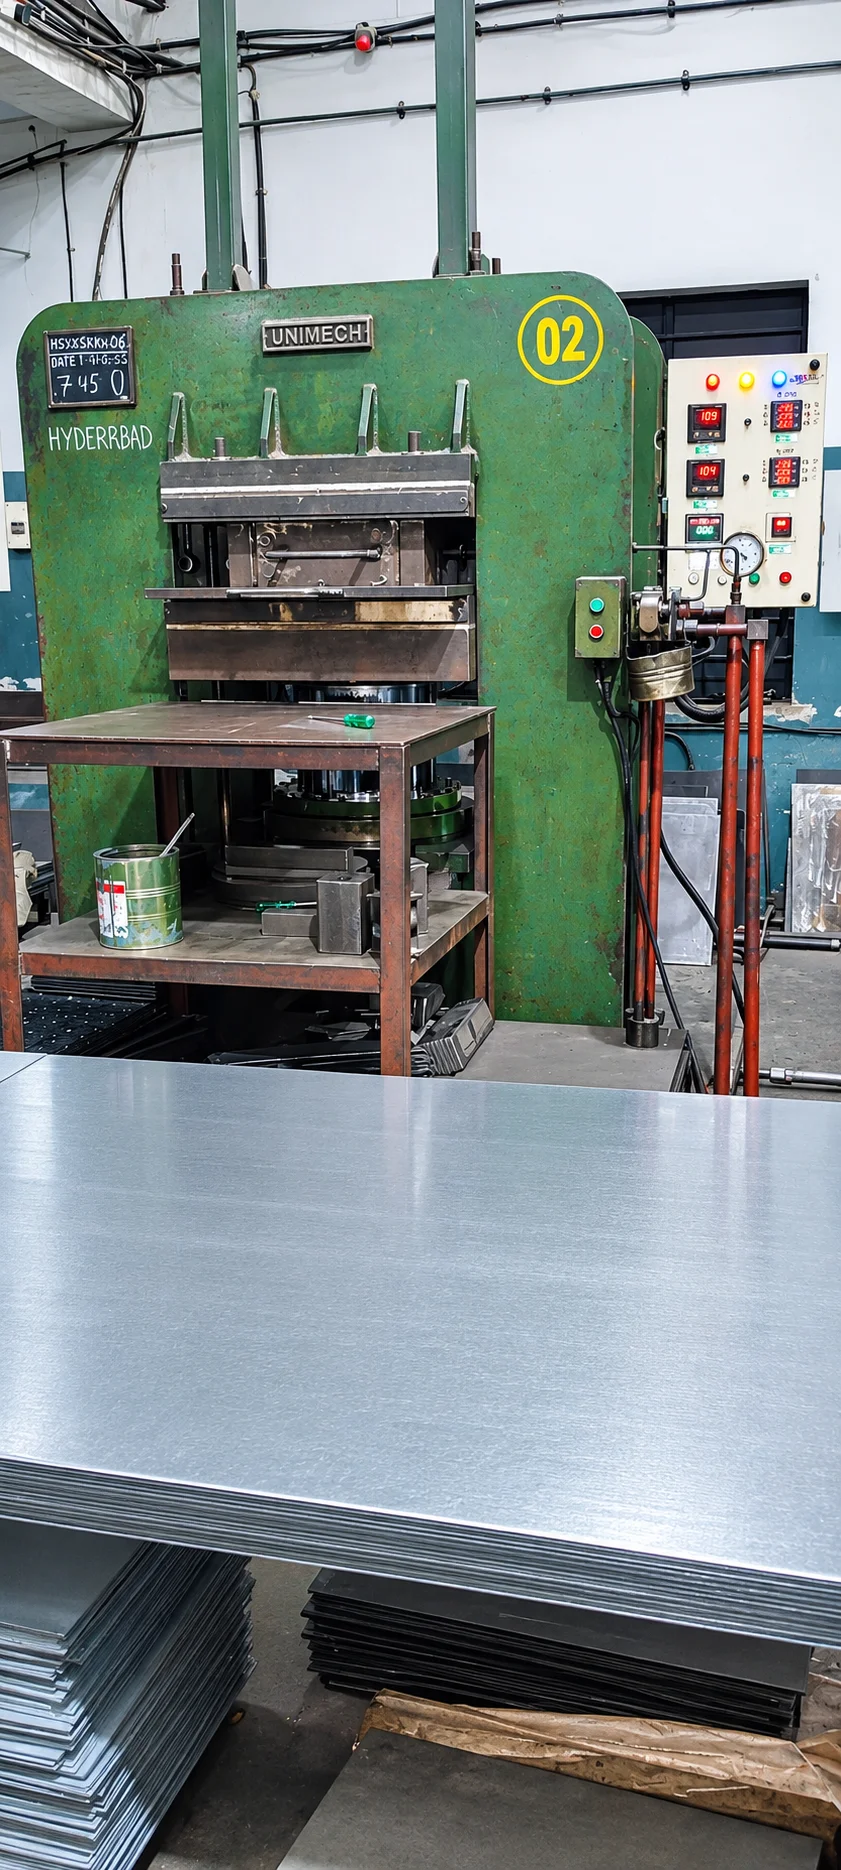
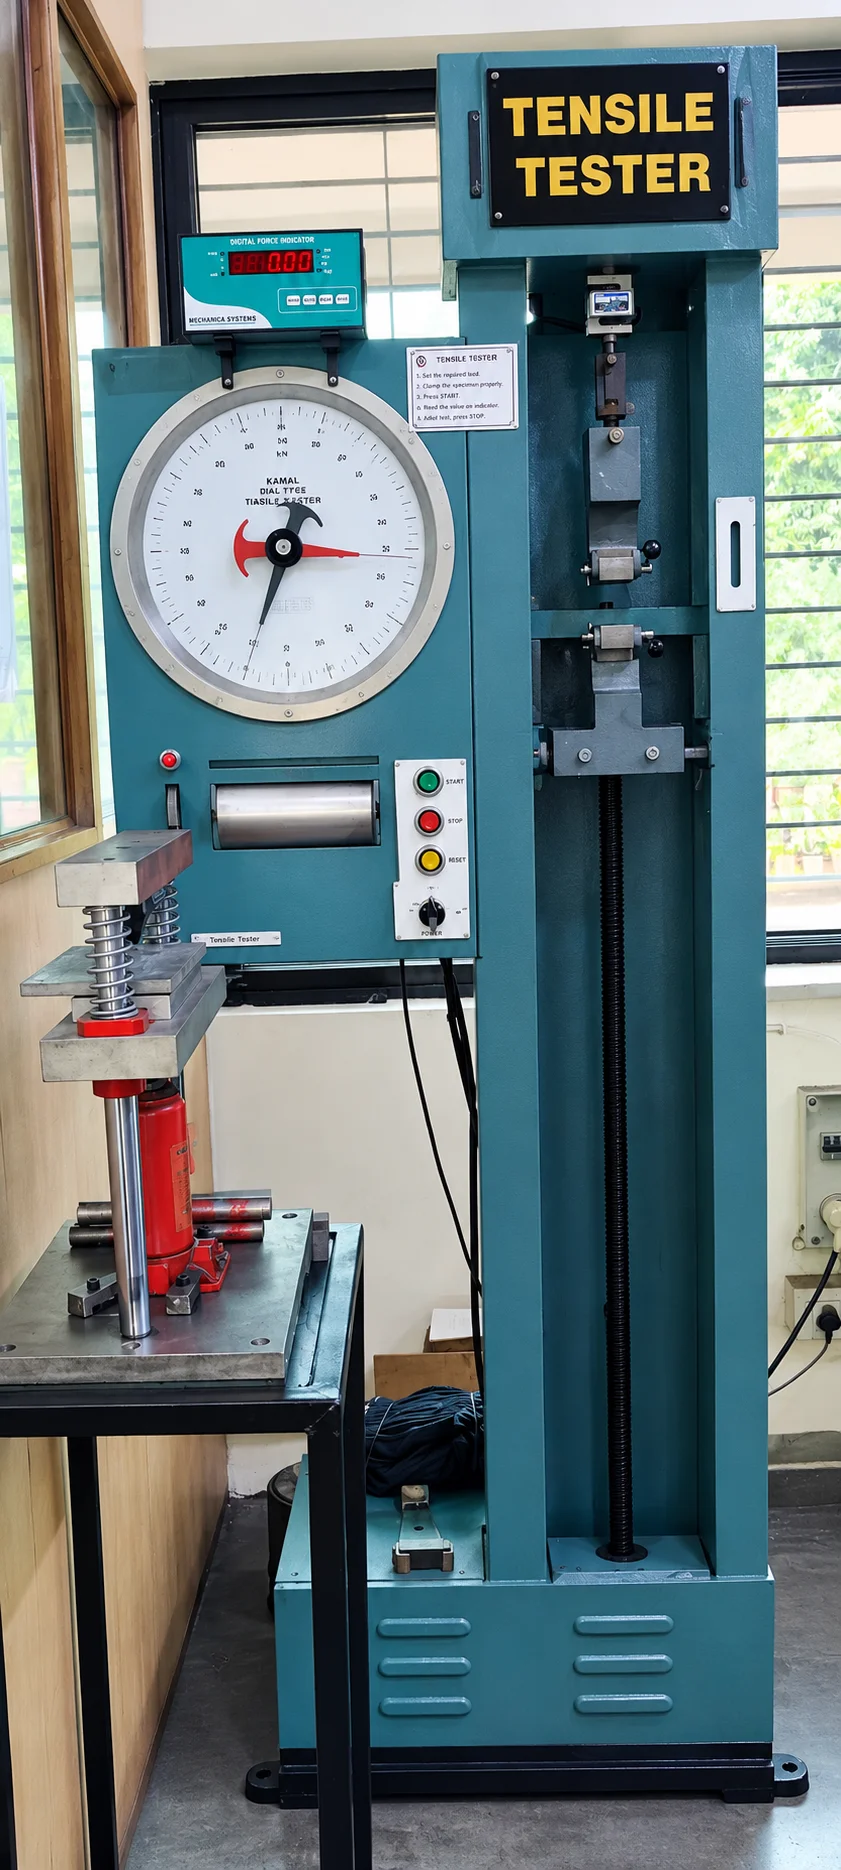
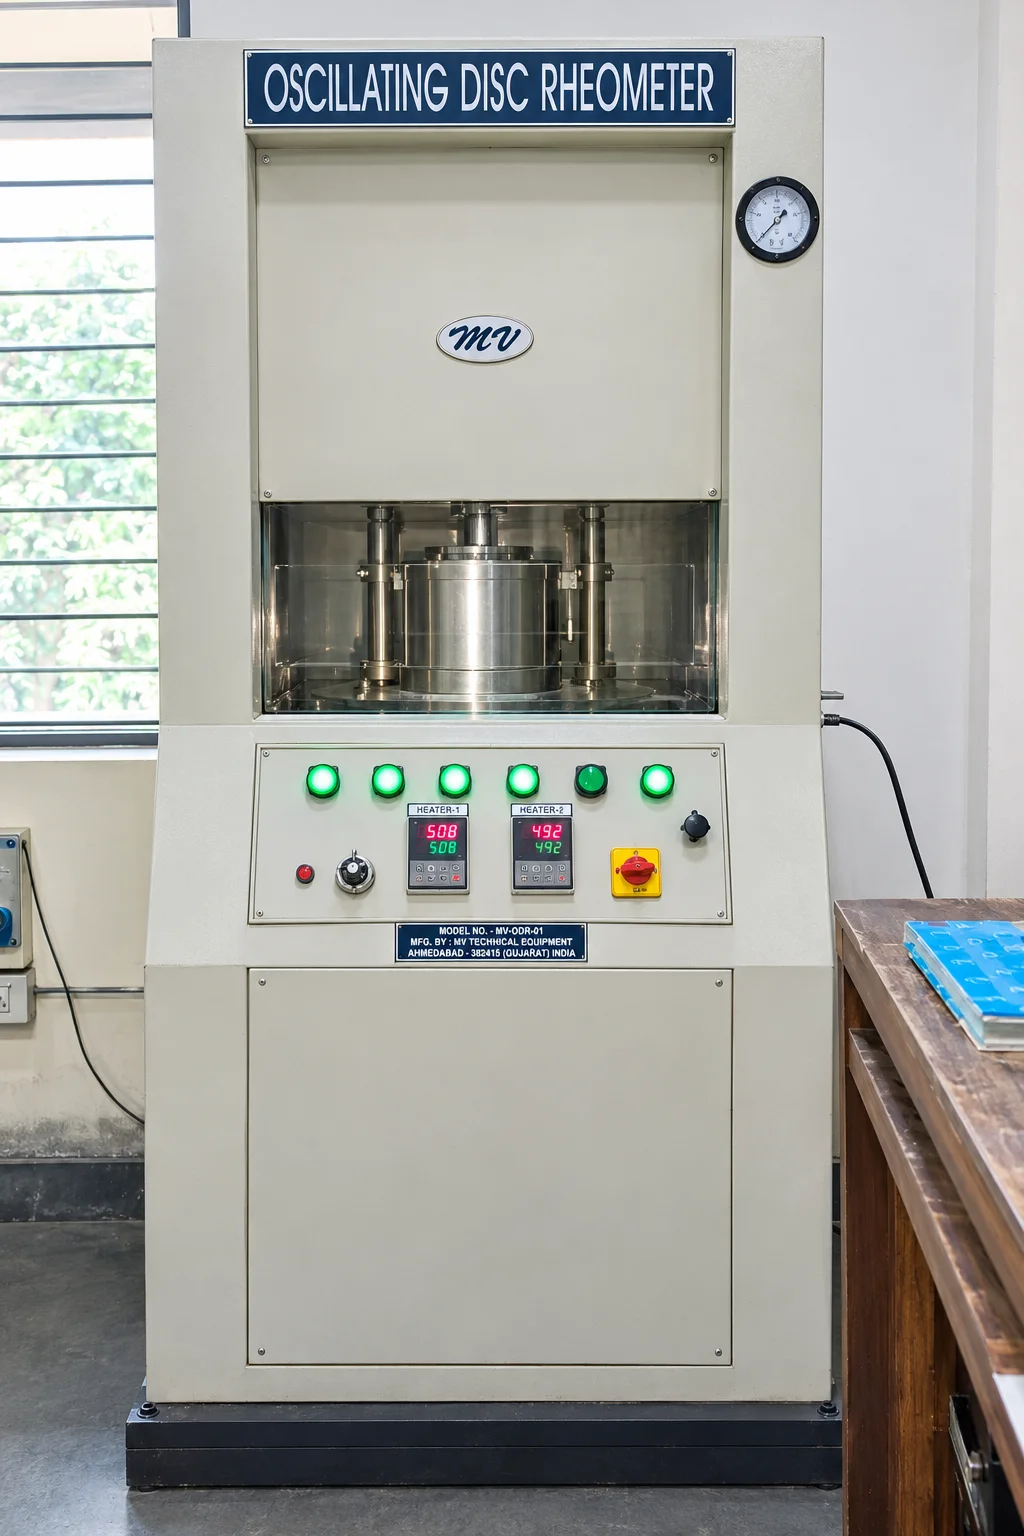
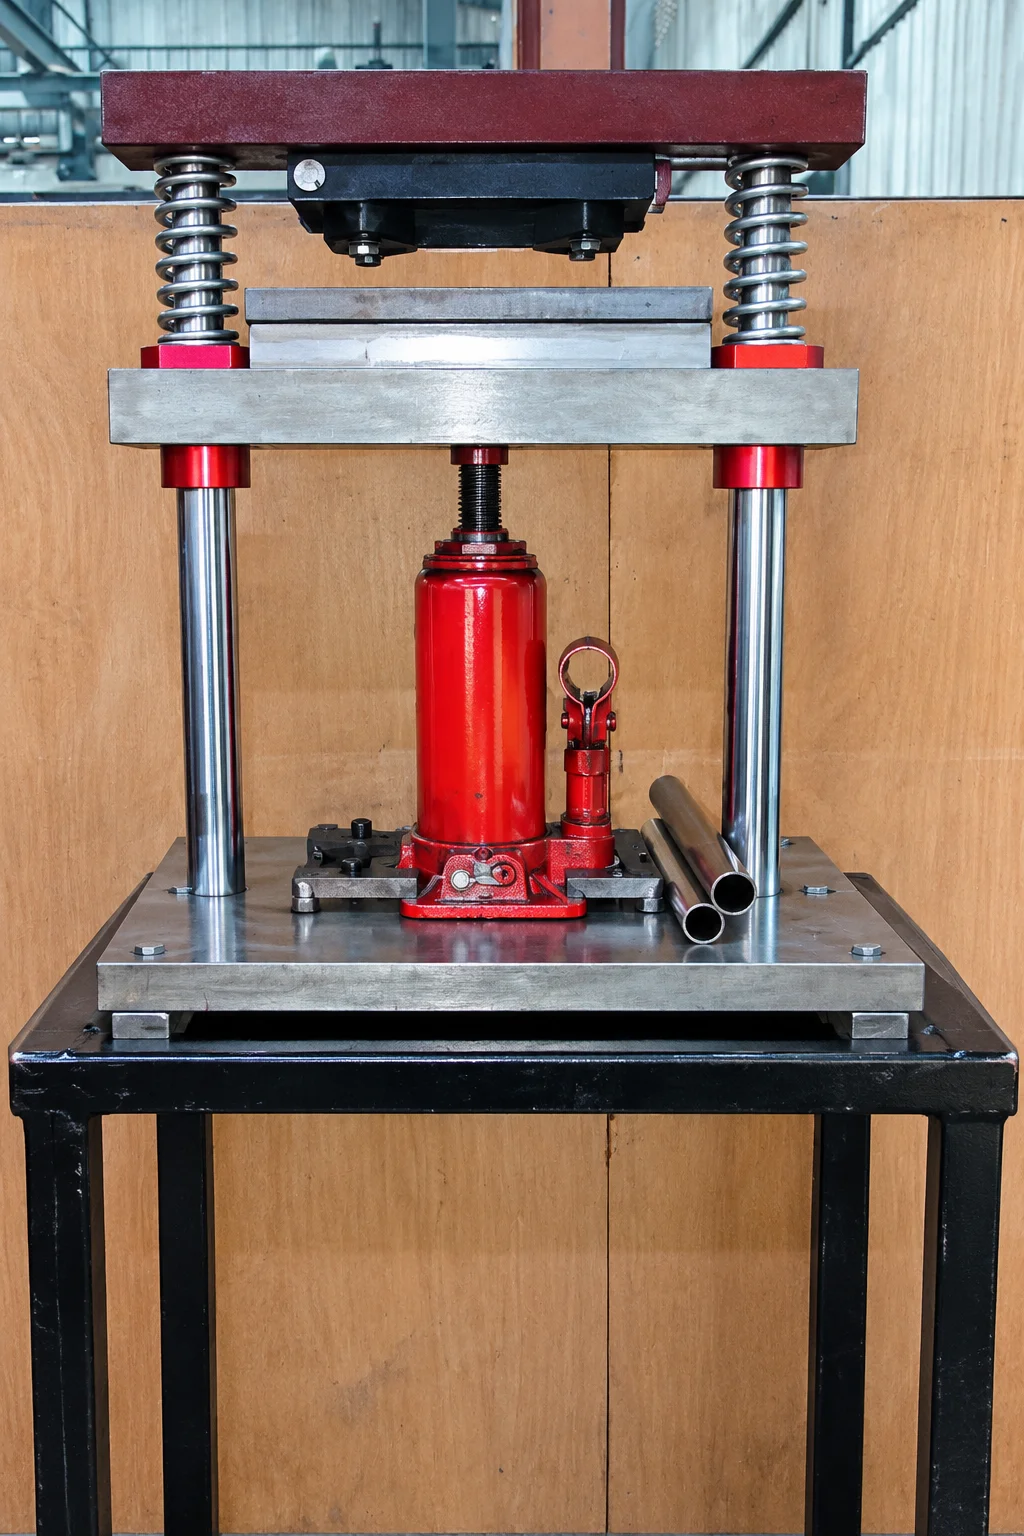
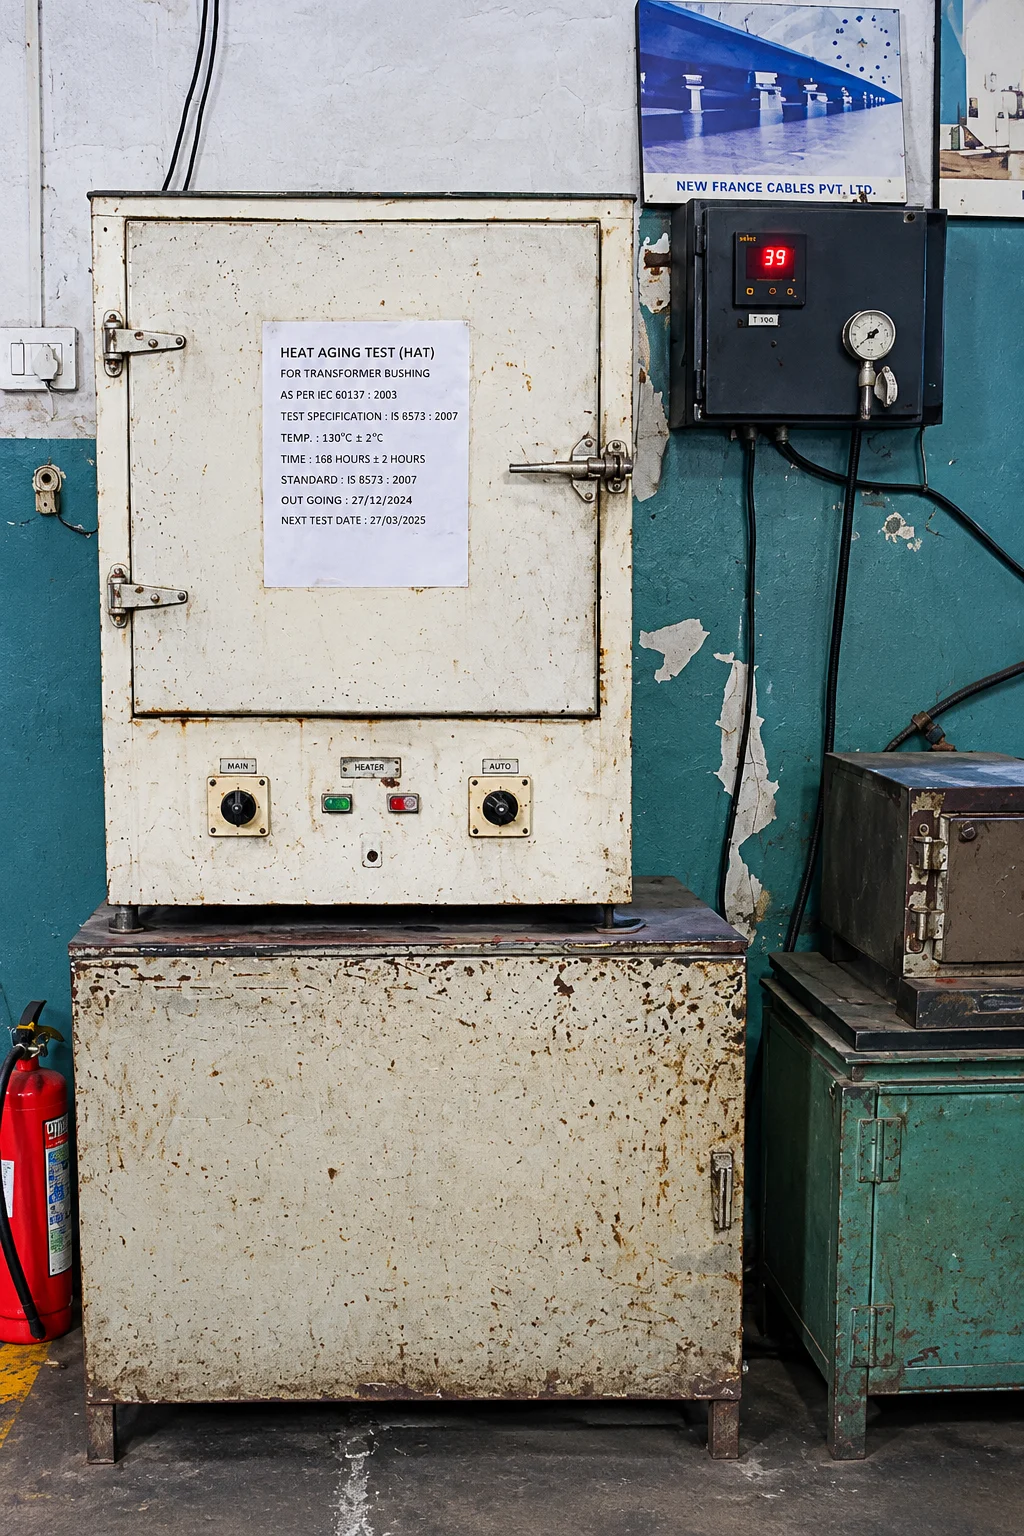
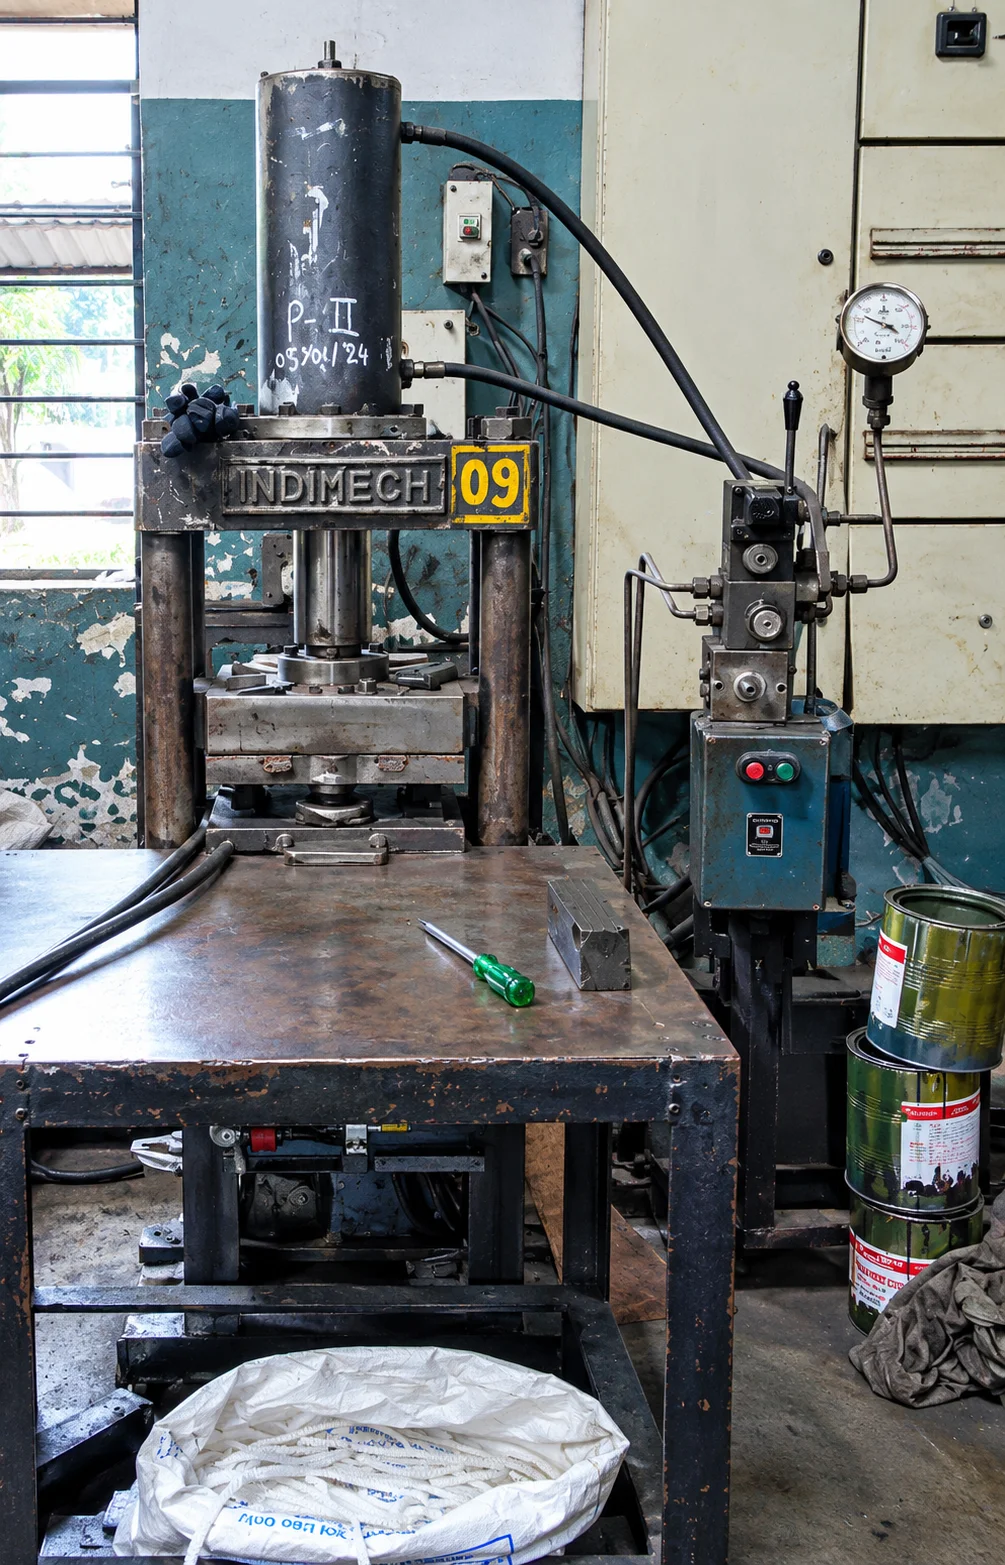
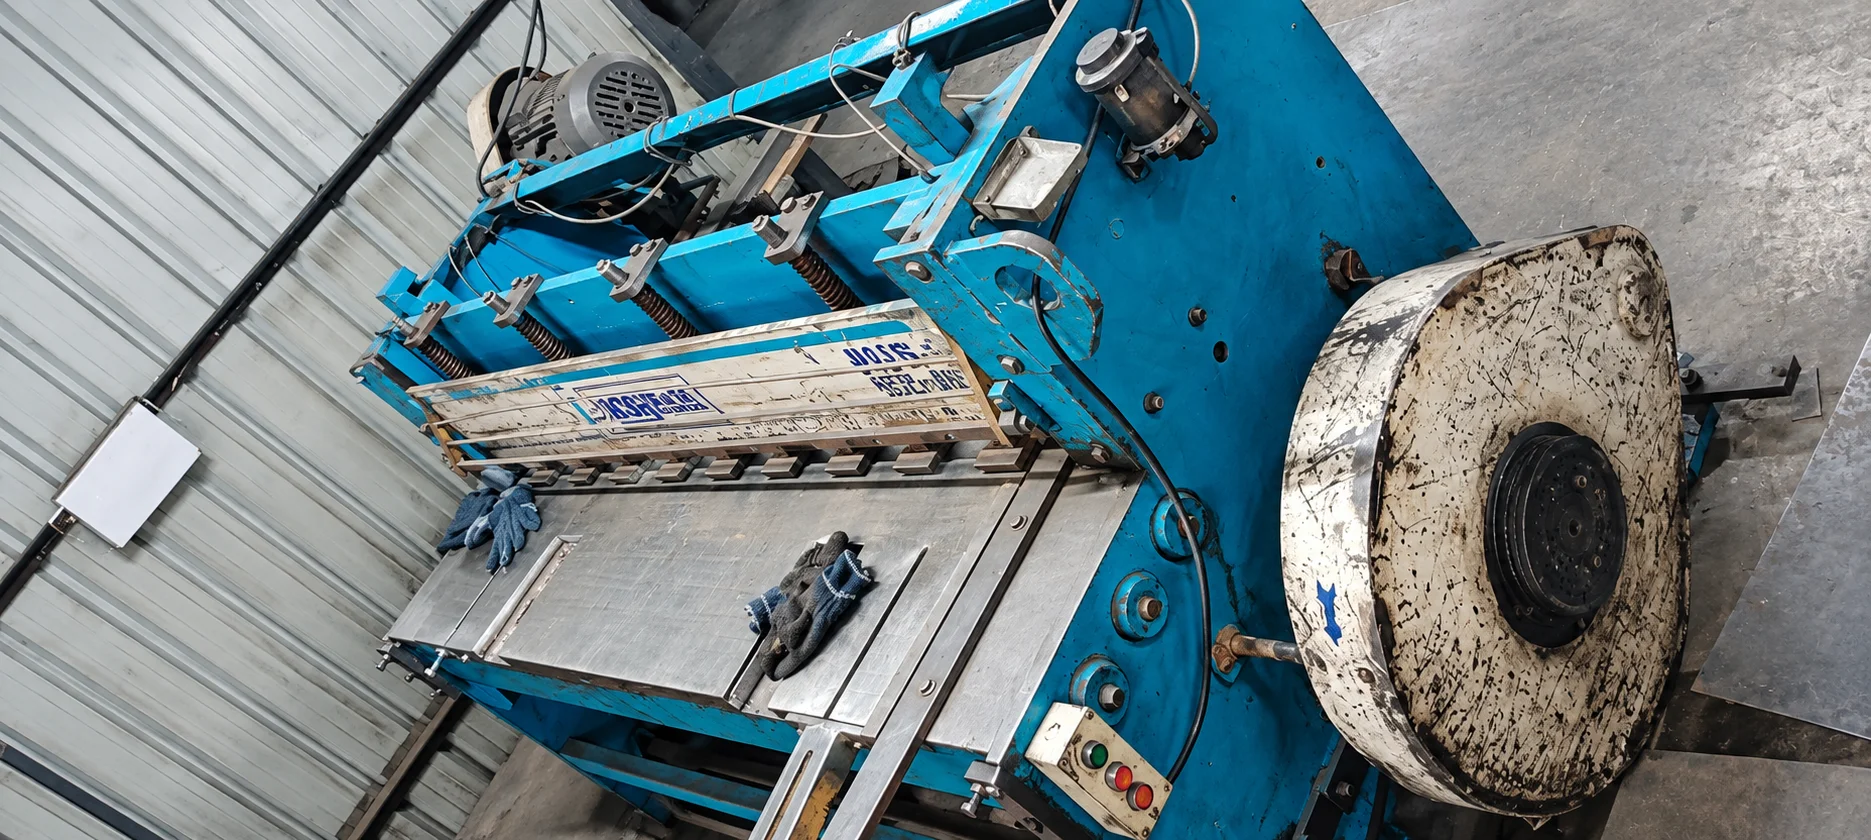
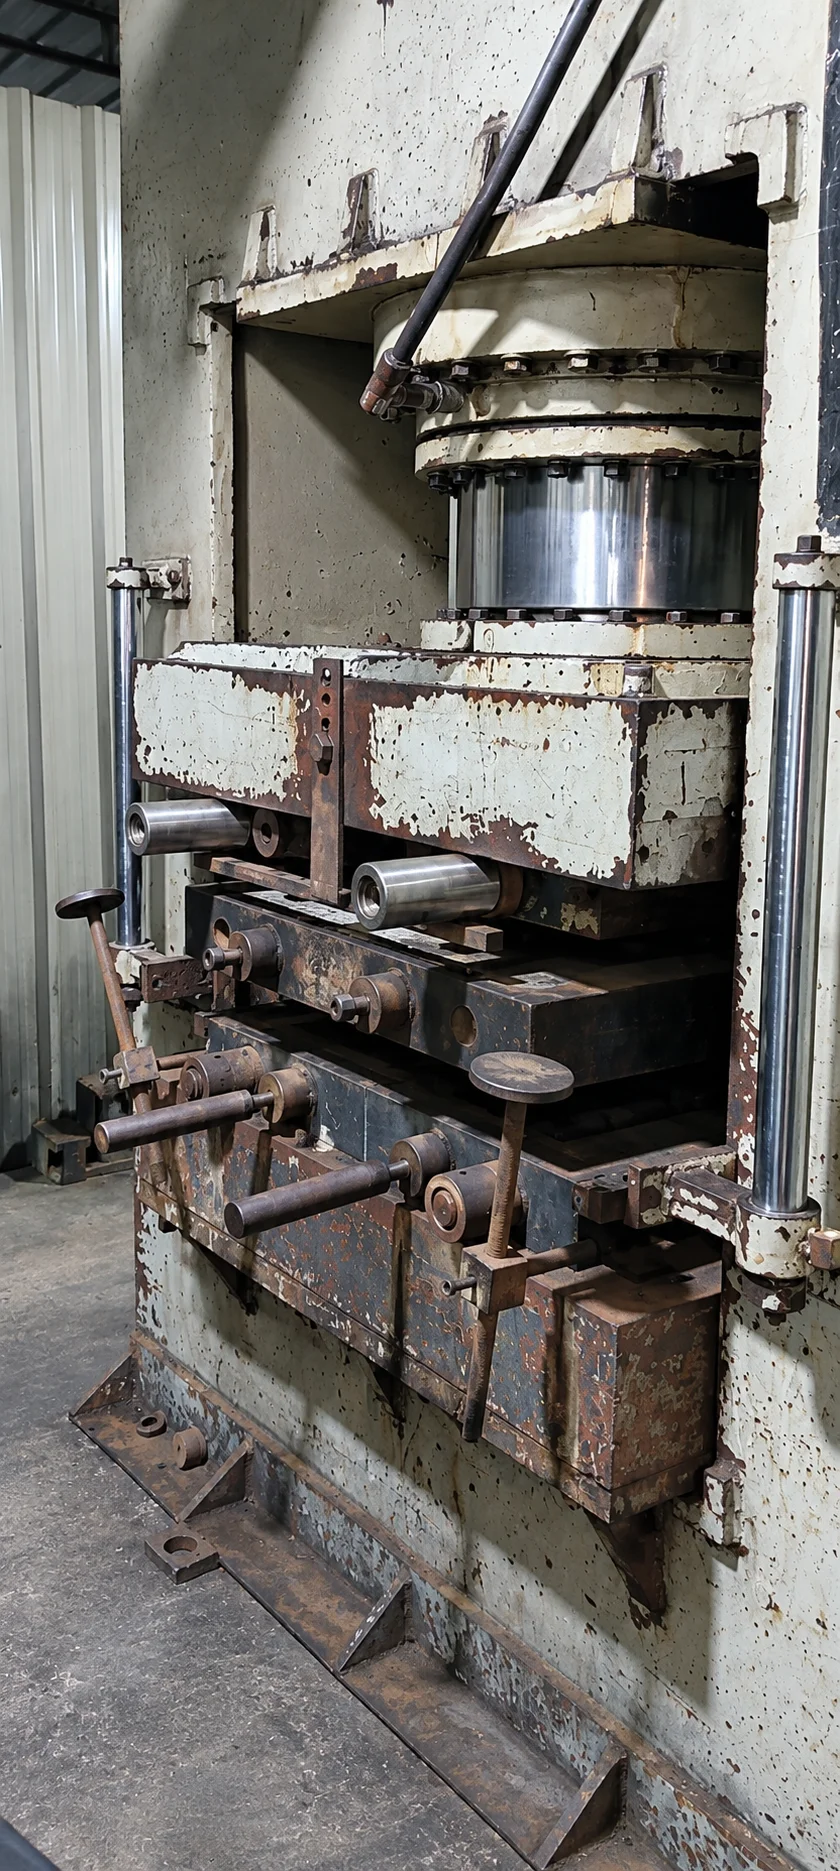
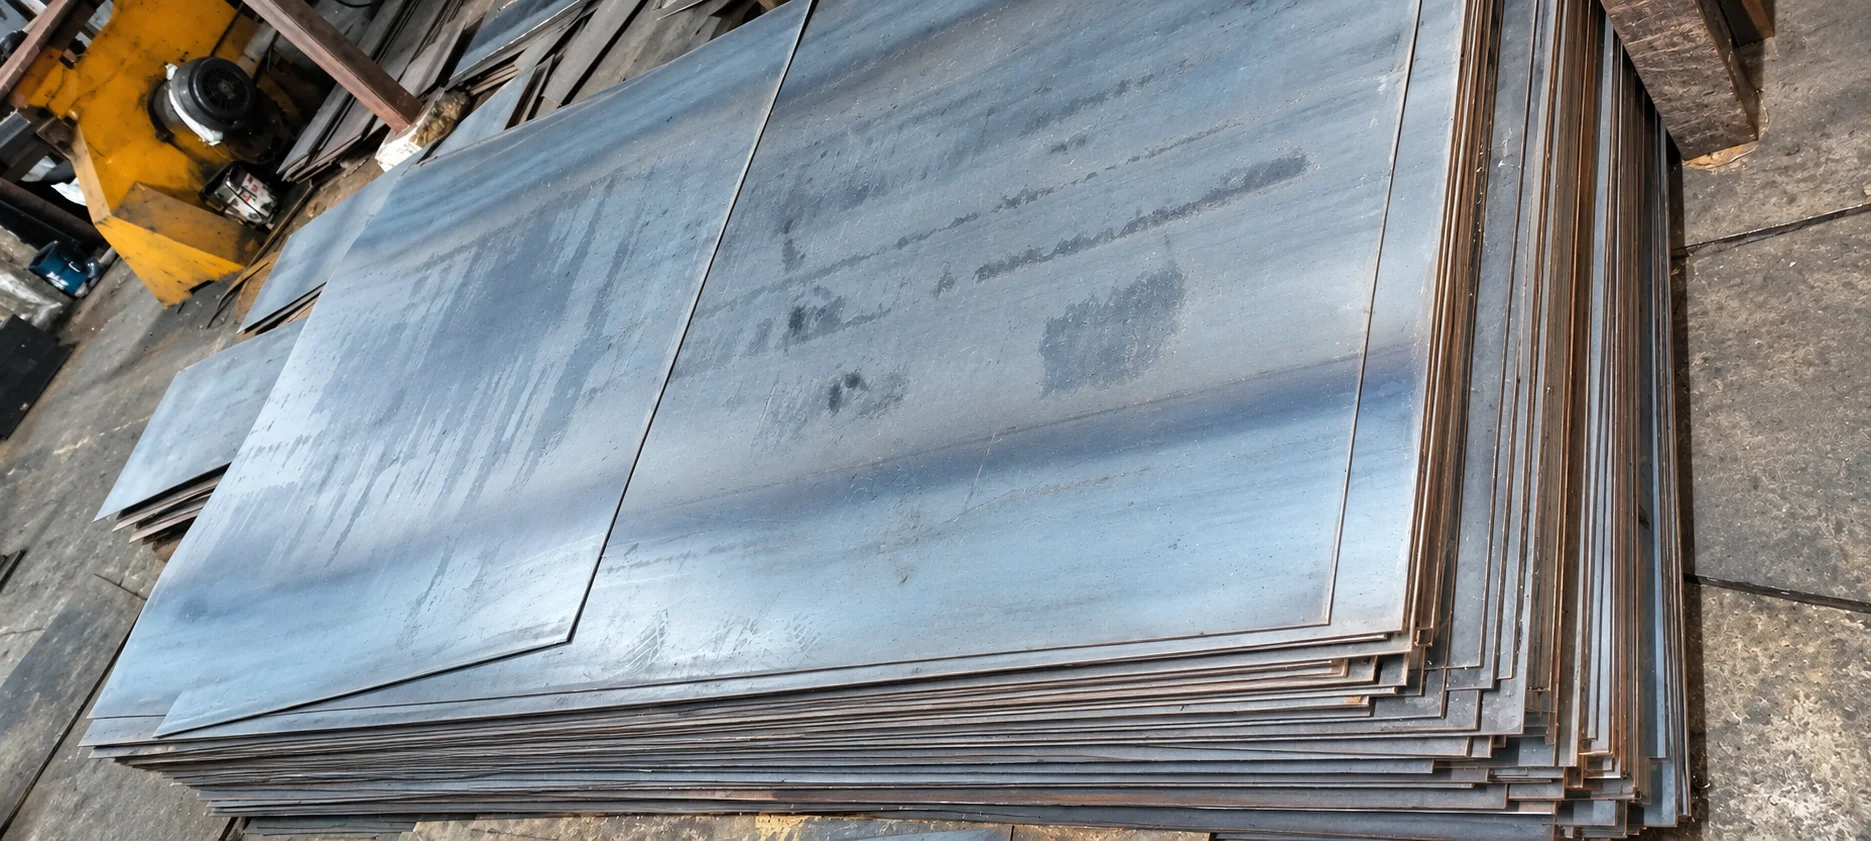
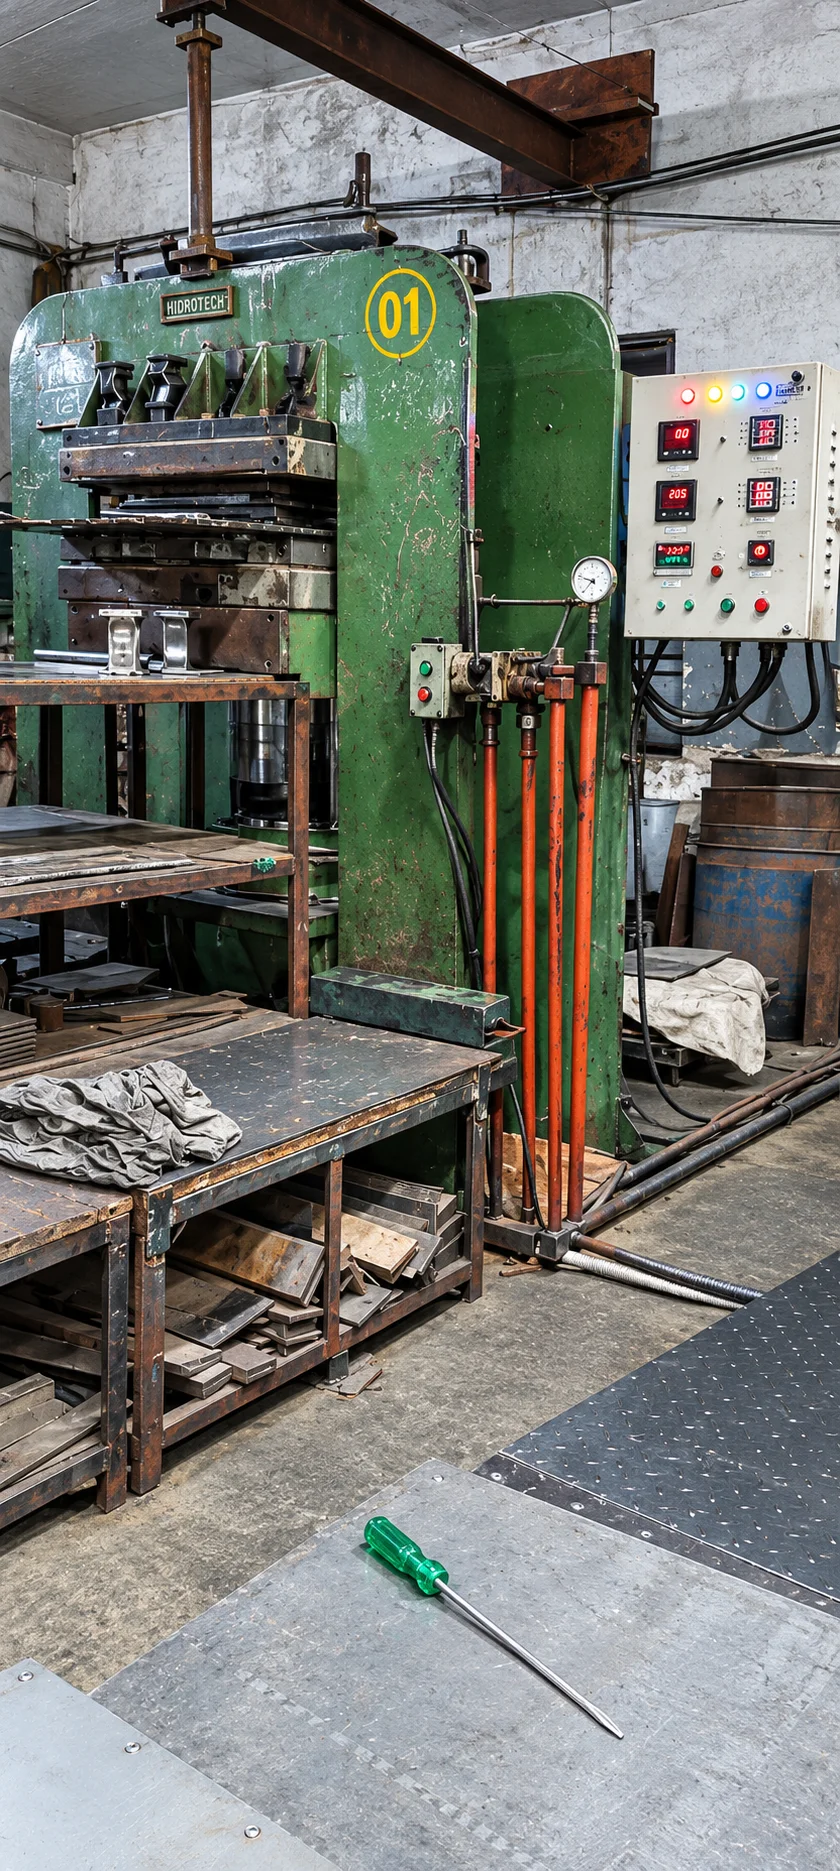
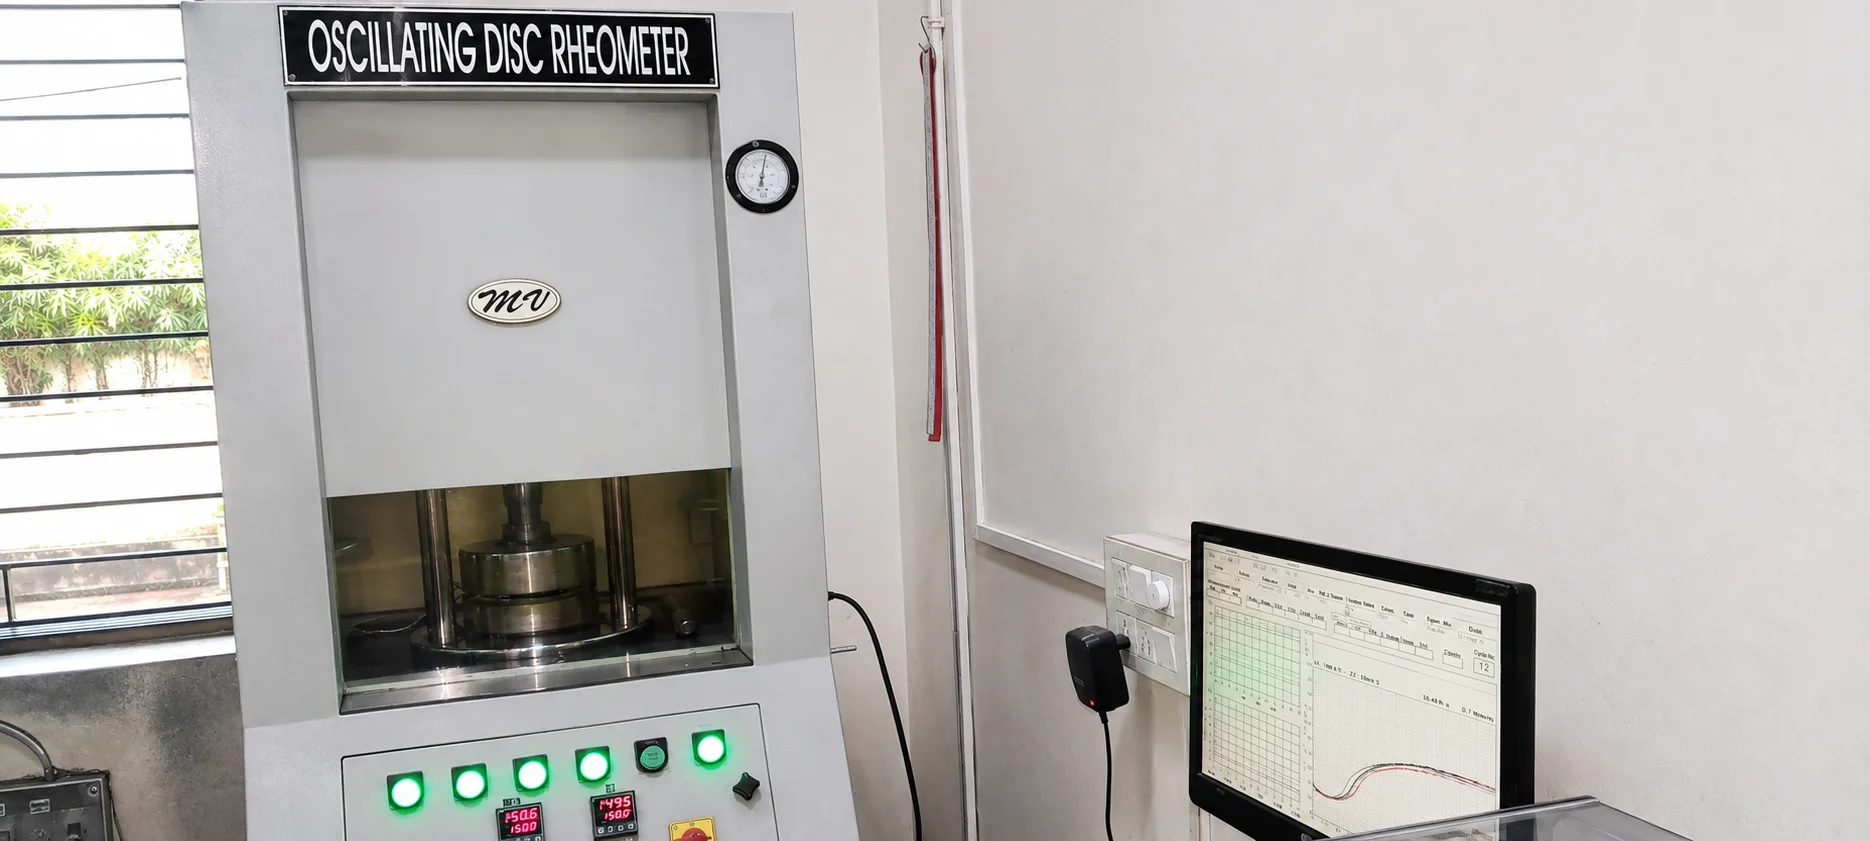
Our Nashik facility is equipped with heavy industrial rubber processing machinery, hydraulic curing presses, grit-blasting stations, and precision testing equipment.
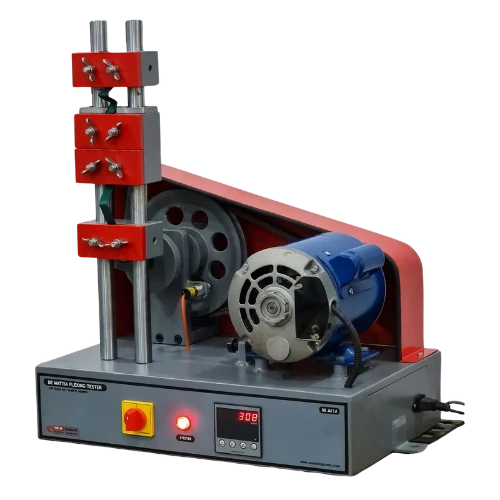
Specialized dynamic flexing and fatigue endurance testing apparatus engineered to evaluate surface crack initiation and cut growth resistance of vulcanized rubber compounds in accordance with ASTM D430, ISO 132, and IS:3400 (Part 8).
| Model Number / Name | IK/DMFT/01 |
|---|---|
| Flexing Frequency | 300 cpm |
| Maximum Opening Between Grips | 75 mm |
| Minimum Opening Between Grips | 10 mm |
| Flexing Angle | 300 cpm |
| Grips | 75 mm (adjustable)/ 57.15 mm (adjustable) |
| Motor Power | 0.5 hp |
| Voltage | 230 v |
| Power Source | Electric |
| Motor | compression set apparatus |
| Power | NIL |
| Color | GOLDEN |
| Sr. No. | Machine Description | Quantity | Capacity / Specifications | Application & Function |
|---|---|---|---|---|
| 1 | Multi-Daylight Hydraulic Vulcanizing Presses | 4 Units | Up to 1200 Metric Tonnes with Digital PLC | Vulcanization & Curing of Elastomeric Bearings |
| 2 | Two-Roll Rubber Mixing Mills | 2 Units | 16" x 42" & 14" x 36" Water Cooled | Elastomer Compounding & Sheeting |
| 3 | Enclosed Shot Blasting Machine | 1 Unit | Sa 2.5 Standard Surface Anchor Profile | Steel Laminate Scale Removal & Surface Prep |
| 4 | Hydraulic Guillotine Shearing Machine | 2 Units | Cuts up to 12mm thick IS:2062 Mild Steel Plates | Steel Laminate Precision Sizing |
| 5 | Precision Bearing Moulds | 50+ Sets | All Standard IRC / RDSO Geometries | Moulding & Dimensional Control |
| 6 | Universal Testing Machine (UTM)-used for Tensile Test, Tear Test ,Elongation and Adhesion. | 1 Unit | Calibrated Electronic UTM with Extensometer | Tensile Strength (≥17 MPa) & Elongation (≥400%) |
| 7 | Thermal Ageing Oven | 1 Unit | Air-circulated Digital Oven (up to 200°C) | 70°C / 72h Thermal Ageing Resistance Tests |
| 8 | Shore A Hardness Tester and Thickness Gauges | Multiple | Calibrated with Master Test Blocks | Routine QC & Stage-Wise Inspection |
| 9 | De Mattia Flex Tester (Model: IK/DMFT/01) | 1 Unit | 300 cpm • 75 mm Opening • 0.5 hp • 230 v Electric (Golden) | Dynamic Rubber Flex Cracking & Cut Growth Resistance (ASTM D430 / ISO 132) |
We welcome third-party inspection agencies (RITES, DNV, EIL, SGS, TUV) and client engineers for stage-wise witness testing at our Nashik plant.